

Wolong High-Voltage Variable Frequency Drive Case Study | South Africa Rio Tinto Mine Project | 3000kW Fan VFD Retrofit
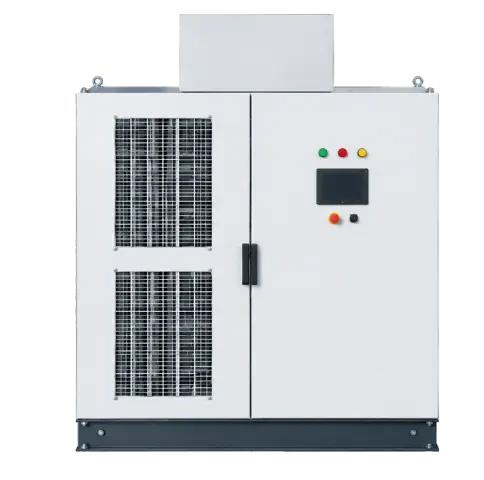
Rio Tinto South Africa Phase2 MVC2 units were commissioned in 2015, and Phase3 MVC2 units in 2015. Located in South Africa, the equipment configuration consists of 3000 kW per unit with 2 units total, driving fan loads. Mine ventilation fans are high-inertia loads. High-voltage variable frequency drives (VFDs) adjust fan speed to meet airflow requirements, reducing throttling losses from dampers. The same-platform HV VFD solution supports runaway start-up, torque limiting, and multi-unit redundant bypass, ensuring reliable operation in harsh mining environments with dust and vibration. Project Value: Continuous commissioning of Phases II and III validated product reliability; fan speed control reduced operational energy consumption; extensive experience delivering projects in overseas mining sectors.
RESULTS
Transformation Results
KEY METRICS
3000kW
2units/issue
Fan
2015-05Start
South Africa
Multiple project phases have been continuously repurchased and commissioned. The wind turbine operates stably with load-adjusted speed control, ensuring long-term reliable performance of the mine ventilation system.
Data Scope and Validation Source: The above metrics are derived from on-site measurements under identical operating conditions before and after the retrofit (comparing energy meter readings with equipment operation logs). The statistical period covers 30 consecutive days of full operation post-retrofit. Motor energy efficiency ratings follow GB 18613-2020 and IEC 60034-30-1, while product efficiency values are cited from the manufacturer's factory test reports. Actual results may vary based on load rate, annual operating hours, and specific operating conditions.
STRUCTURED LINKS
Related Products & Industries
RELATED
Products and Solutions in this Project

Flotation Machine Drive Control
Flotation Cell Drive and Control System Solution
The TYCP5 series flotation machine utilizes a low-speed permanent magnet motor for direct drive of the impeller, replacing the traditional "induction motor + pulley + belt" transmission system. Paired with WD200 high-performance vector inverters, ECC variable frequency control cabinets, and system control cabinets, it can optionally connect to the iMotorLinx Shunzhi Cloud industrial internet platform. Under an 8kW load condition (8), total transmission efficiency increases from 76% to 90.5%, achieving energy savings of up to 16.1%.

Permanent Magnet Drum Drive Control
Permanent Magnet Drum Drive Control System Solution
A permanent magnet electric drum direct-drive system solution for belt conveyors in mining, chemical, and building materials industries. Replacing traditional drive systems with gear reducers and asynchronous motors, the STY series permanent magnet direct-drive drums are paired with WD200 series high-performance universal variable frequency drives and energy feedback units, Wolong Shunyun IoT modules and PLCs, advanced wireless temperature-vibration integrated sensors, and the Wolong iMotorLinx Shunzhi Cloud industrial internet platform to achieve simplified transmission chains, S-curve smooth starts, precise speed-torque control, and energy recovery.
SOLUTIONS
Recommended related solutions
Motor replacement solutions
Address challenges such as aging equipment, motor maintenance needs, and high procurement costs. Leveraging motor parameters, mechanical dimensions, and actual operating conditions, we provide 1 compatible industrial motor replacement solutions for 1, requiring no structural modifications to your equipment.
Permanent Magnet/Synchronous Reluctance Motor Energy Efficiency Retrofit
Replace traditional induction motors with permanent magnet synchronous motors (PMSM) or permanent magnet reluctance motors (PMRM). Optimize motor-load matching based on operating conditions to reduce energy consumption and improve operational stability.

Industrial Energy Saving Solutions Consultation
Factory-wide motor system energy-saving diagnostics and retrofit planning, delivering phased implementation roadmaps and ROI projections.
More Cases
View All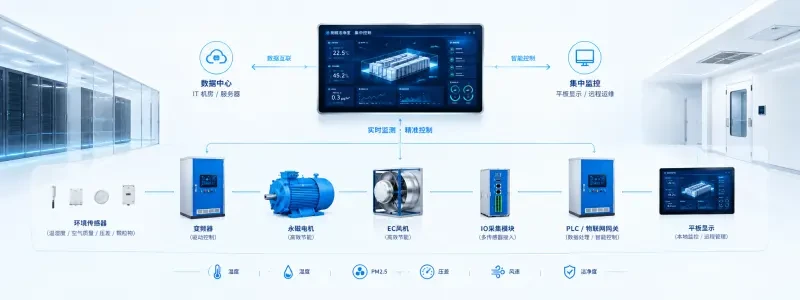
Panpu EC Permanent Magnet Fan Case | Cleanroom Operator | Energy-Saving Retrofit of Cleanroom Fan Clusters with On-Demand Speed Control
Replace traditional AC fan clusters with EC permanent magnet fans, and use differential pressure sensing to enable on-demand speed control for air supply, reducing energy consumption and noise in the cleanroom's ventilation system.
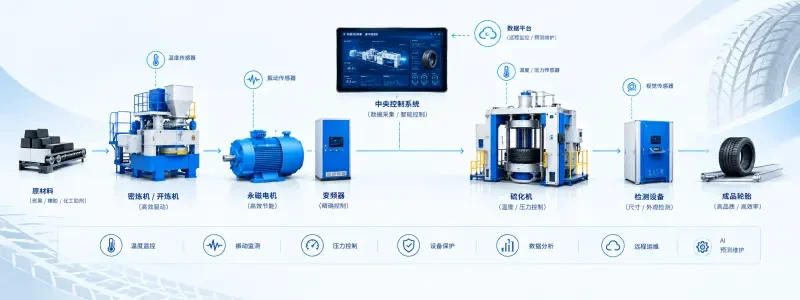
Panpu Permanent Magnet Direct Drive Motor Case: Kiri Chemical Rubber Tire Factory – Whole-Line Drive System Energy Efficiency Retrofit for Tire Production Line
Optimize the motor drive system across the entire tire production line, coordinate multi-device control to reduce overall energy consumption, and adapt to wheel control and molding processes. Help factories achieve energy savings, carbon reduction, and improved production efficiency.

28 0KW Permanent Magnet Motor + VFD Case Study | SCM Chemical Fiber | Large-Scale Process Equipment Retrofit for Energy Efficiency
Equipped with a 280kW permanent magnet motor and dedicated variable frequency drive (VFD), this integrated solution optimizes load performance, reduces energy consumption, and enhances operational stability. It delivers complete case study support to help large-scale process equipment achieve cost reduction and efficiency gains.
Looking for a motor and energy-saving solution tailored to your operating conditions?
Submit request. Our technical engineer will contact you within 1 business days.